HUASHENG PRECISION · Updated November 15, 2026
Sheet Metal Bend Radius Chart by Material: Minimum R/t and K-Factor
Published minimum inside bend radii for common sheet materials, given as a multiple of sheet thickness (R/t), with the source of every value. These are reference values from mills, distributors and material standards, not our manufacturing limits. The radius a part can actually take also depends on thickness, bend direction, tooling and the forming method.
Minimum bend radius by material (published values)
R is the inside radius and t is the sheet thickness. Each table states where its values come from and what kind of value it is: a forming recommendation, a mill datasheet minimum or a bend-test requirement in a material standard. They are not interchangeable.
Aluminum sheet: 90° cold bend
Swipe horizontally to read the table.
| Alloy-temper | 1/64 in (0.4 mm) | 1/32 in (0.8 mm) | 1/16 in (1.6 mm) | 1/8 in (3.2 mm) |
|---|---|---|---|---|
| 1100-H14 | 0 | 0 | 0 | 1t |
| 3003-H14 | 0 | 0 | 0 | 1t |
| 5052-O | 0 | 0 | 0 | ½t |
| 5052-H32 | 0 | 0 | 1t | 1½t |
| 5052-H34 | 0 | 1t | 1½t | 2t |
| 6061-O | 0 | 0 | 0 | 1t |
| 6061-T4 | 0 | 0 | 1t | 1½t |
| 6061-T6 | 1t | 1t | 1½t | 2½t |
| 2024-T3 | 2½t | 3t | 4t | 5t |
| 7075-T6 | 3t | 4t | 5t | 6t |
Source: United Aluminum, Recommended Minimum Bend Radii for 90-Degree Cold Forming of Sheet. The source states these are the minimum recommended radii for bending without fracturing in a standard press brake with air-bend dies, that other bending operations may require larger or permit smaller radii, and that the minimum also varies with the design and condition of the tooling. Millimetre thicknesses are our conversion.
Carbon, HSLA and dual-phase steel sheet: 90° bend
Swipe horizontally to read the table.
| Specification and grade | Inside radius | Kind of value |
|---|---|---|
| ASTM A1011 hot-rolled, SS Grade 30 and 33 | 1t | Suggested minimum, nonmandatory appendix |
| ASTM A1011 hot-rolled, SS Grade 36 Type 1 | 1½t | Suggested minimum, nonmandatory appendix |
| ASTM A1011 hot-rolled, SS Grade 36 Type 2 and Grade 40 | 2t | Suggested minimum, nonmandatory appendix |
| ASTM A1011 hot-rolled, SS Grade 50 | 2½t | Suggested minimum, nonmandatory appendix |
| ASTM A1011 hot-rolled, HSLAS Grade 50 Class 1 / Class 2 | 2t / 1½t | Suggested minimum, nonmandatory appendix |
| ASTM A1011 hot-rolled, HSLAS-F Grade 50 | 1t | Suggested minimum, nonmandatory appendix |
| ASTM A1008 cold-rolled, SS Grade 33 | 1½t | Suggested minimum, nonmandatory appendix |
| ASTM A1008 cold-rolled, SS Grade 40 | 2t | Suggested minimum, nonmandatory appendix |
| ASTM A1008 cold-rolled, SS Grade 50 | 2½t | Suggested minimum, nonmandatory appendix |
| ASTM A1008 cold-rolled, HSLAS-F Grade 50 | 1t | Suggested minimum, nonmandatory appendix |
| Docol CR330Y590T-DP (DP590), uncoated | 0.0 × t | Mill datasheet minimum |
| Docol CR330Y590T-DP (DP590), GI / GA / ZA coated | 1.2 × t | Mill datasheet minimum |
| Docol CR440Y780T-DP (DP780), uncoated | 1.0 × t | Mill datasheet minimum |
| Docol CR440Y780T-DP (DP780), GI / GA / ZA coated | 1.8 × t | Mill datasheet minimum |
| Docol CR590Y980T-DP (DP980), uncoated / EG | 2.0 × t | Mill datasheet minimum |
| Docol CR590Y980T-DP (DP980), GI / GA / ZA coated | 3.0 × t | Mill datasheet minimum |
Sources: ASTM A1011 and A1008 appendix values as listed by American Steel & Aluminum (A1011, A1008), which notes that a bend line parallel to the rolling direction is the harder way to bend. Dual-phase values are from the SSAB Docol product pages (600DP, 800DP, 1000DP); SSAB adds that a tight radius may cause micro-cracking of the coating and encourages a larger radius where the design permits. The listed tables do not give a value for commercial steel (CS) or drawing steel (DS); confirm those with the producer.
Stainless steel and titanium: bend-test requirements in ASTM standards
These are acceptance tests a mill product must pass, not forming recommendations for a production part. They show what the material is required to withstand.
Swipe horizontally to read the table.
| Material, annealed | Thickness | Requirement as stated | Equivalent inside radius |
|---|---|---|---|
| 304 | up to 0.1874 in (4.76 mm) | 180° free bend, mandrel diameter 1 × t | 0.5t |
| 304L, 316, 316L | up to 0.050 in (1.27 mm) | 180° free bend, mandrel diameter 1 × t | 0.5t |
| 304L, 316, 316L | over 0.050 to 0.1874 in (1.27 to 4.76 mm) | 180° free bend, mandrel diameter 2 × t | 1t |
| Titanium Grade 2 | under 0.070 in (1.8 mm) | 105° bend, mandrel radius 2T | 2t |
| Titanium Grade 2 | 0.070 to 0.187 in (1.8 to 4.75 mm) | 105° bend, mandrel radius 2.5T | 2.5t |
| Titanium Grade 5 (Ti-6Al-4V) | under 0.070 in (1.8 mm) | 105° bend, mandrel radius 4.5T | 4.5t |
| Titanium Grade 5 (Ti-6Al-4V) | 0.070 to 0.187 in (1.8 to 4.75 mm) | 105° bend, mandrel radius 5T | 5t |
Sources: ASTM A666-10, Table 3 (free bend requirements, annealed) and ASTM B265-08b, Table 1 (bend test, radius of mandrel). A666 states a mandrel diameter, so the radius column is half of it and is our arithmetic. Later editions of either standard may differ; check the edition named on your order.
Copper and brass strip up to 0.5 mm: 90° bend ratio r/t
Swipe horizontally to read the table.
| Cu-ETP / C11000 temper | Bend axis across rolling direction | Bend axis parallel to rolling direction |
|---|---|---|
| R220 | 0 | 0 |
| R240 | 0 | 0 |
| R290 | 0 | 0.5 |
| R360 | 1 | 2 |
| CuZn30 / C26000 temper | Bend axis across rolling direction | Bend axis parallel to rolling direction |
|---|---|---|
| R270 | 0 | 0 |
| R350 | 0 | 0 |
| R410 | 0 | 0 |
| R480 | 0 | 1 |
| R550 | 0.5 | 2 |
| R630 | 1 | 3 |
Sources: Aurubis strip datasheets for Cu-ETP (C11000) and CuZn30 (C26000). Tempers are EN designations by tensile strength; R220 and R270 are the softest listed. The values apply to strip up to 0.5 mm thick and should not be carried over to thicker sheet.
Use the material’s own datasheet for the exact alloy, temper, thickness and bend direction when a radius is close to these values.
Convert R/t into an inside radius
R is the inside radius and t is the sheet thickness. This is a dimension conversion table, not a table of minimum allowable radii or a statement of our manufacturing limits.
Swipe horizontally to read the table.
| Thickness t | R/t = 0.5 | R/t = 1 | R/t = 2 | R/t = 3 |
|---|---|---|---|---|
| 0.5 mm | 0.25 mm | 0.5 mm | 1 mm | 1.5 mm |
| 1 mm | 0.5 mm | 1 mm | 2 mm | 3 mm |
| 1.5 mm | 0.75 mm | 1.5 mm | 3 mm | 4.5 mm |
| 2 mm | 1 mm | 2 mm | 4 mm | 6 mm |
| 3 mm | 1.5 mm | 3 mm | 6 mm | 9 mm |
For example, 2 mm sheet with an inside radius of 3 mm has R/t = 1.5. “R3” is not the same as “three times the thickness”. Identify outside-radius requirements and the finished angle separately.
Check the exact material before choosing a minimum radius
Swipe horizontally to read the table.
| Material family | What to confirm |
|---|---|
| 5052 and other aluminum sheet | Alloy, temper, sheet thickness and rolling direction. Do not transfer a limit between tempers. |
| 6061-T6 and other heat-treated aluminum | Condition during forming and required final condition. Review a tight radius against supplier guidance for that condition. |
| SPCC, SECC, SGCC and similar sheet | Grade, strength class, thickness, coating and cosmetic acceptance. |
| 304 / 316 stainless | Supply condition, rolling direction, thickness and springback. A grade name alone does not define one minimum radius. |
| High-strength sheet steel | Exact grade, strength class, thickness and bend direction in the supplier recommendations. |
| Copper and brass | Material designation and hardness / temper. Assess hemming separately from an ordinary bend. |
Show the bend axis relative to rolling direction. Acceptance may include the finished angle, surface appearance, hole distortion and function as well as the absence of cracking.
K-factor and the flat pattern
K-factor is the offset of the neutral axis from the inside surface divided by sheet thickness. It must correspond to the forming conditions; a material name alone does not establish a universal value. Identify the bend table or K-factor used if you supply a flat pattern.
- Supply the finished shape, inside radii and finished angles; keep the flat pattern and model at the same revision.
- Distinguish bend allowance, the neutral-axis length through the bend, from bend deduction used with outside flange dimensions.
- Confirm unfolding responsibility and resolve differences between the supplied flat pattern and the finished drawing before cutting.
Bend allowance and bend deduction formulas
- Bend allowance: BA = π × (R + K × T) × A / 180, where R is the inside radius, T the thickness and A the angle through which the material is bent, in degrees.
- Outside setback: OSSB = tan(A / 2) × (R + T).
- Bend deduction: BD = 2 × OSSB − BA.
Generic K-factor chart
Swipe horizontally to read the table.
| Method and inside radius | Soft materials | Medium materials | Hard materials |
|---|---|---|---|
| Air bending, 0 to 1 × thickness | 0.33 | 0.38 | 0.40 |
| Air bending, 1 to 3 × thickness | 0.40 | 0.43 | 0.45 |
| Air bending, over 3 × thickness | 0.50 | 0.50 | 0.50 |
| Bottoming, 0 to 1 × thickness | 0.42 | 0.44 | 0.46 |
| Bottoming, 1 to 3 × thickness | 0.46 | 0.47 | 0.48 |
| Bottoming, over 3 × thickness | 0.50 | 0.50 | 0.50 |
| Coining, 0 to 1 × thickness | 0.38 | 0.41 | 0.44 |
| Coining, 1 to 3 × thickness | 0.44 | 0.46 | 0.47 |
| Coining, over 3 × thickness | 0.50 | 0.50 | 0.50 |
Source: The Fabricator, Analyzing the k-factor in sheet metal bending, a generic chart based on information from Machinery’s Handbook. In the original chart the soft and medium columns are headed aluminum and the hard column steel. The same article gives 0.4468 as the average used for most bending applications.
Machinery’s Handbook 90° bend formulas, including copper and brass
Swipe horizontally to read the table.
| Material group | Length of stock in a 90° bend | Corresponding K-factor |
|---|---|---|
| Soft brass, soft copper | L = 0.55 × T + 1.57 × R | about 0.35 |
| Half-hard copper and brass, soft steel, aluminum | L = 0.64 × T + 1.57 × R | about 0.41 |
| Bronze, hard copper, cold-rolled steel, spring steel | L = 0.71 × T + 1.57 × R | about 0.45 |
Source: Machinery’s Handbook, 31st edition, p. 1421. The handbook gives the formulas, not a K-factor; the last column is our calculation (coefficient divided by π/2). The handbook applies these formulas to parts bent with simple tools or on the bench.
A published K-factor is a starting value. The Fabricator describes deriving the K-factor from at least three test pieces of the same material grade and thickness, bent under the same conditions and grain direction.
Holes, short flanges and springback
- State whether a hole distance is measured to its centre or edge, and to a bend line or tangent. Include the hole size.
- Nearby holes and slots require distortion review; possible changes to location, relief or operation sequence need design approval.
- Short flanges, multiple bends and box shapes require a review of tool support and interference.
- Specify the finished angle after unloading. Springback compensation depends on material and forming conditions; do not prescribe one correction for every grade.
Sheet metal equipment and manufacturing samples
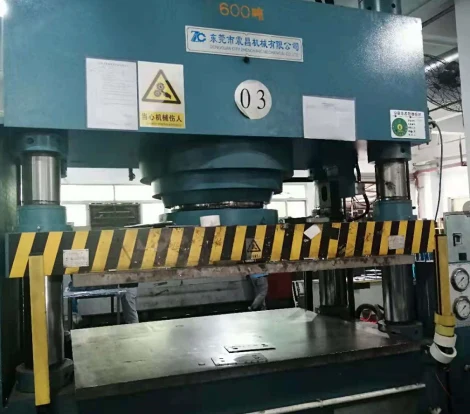
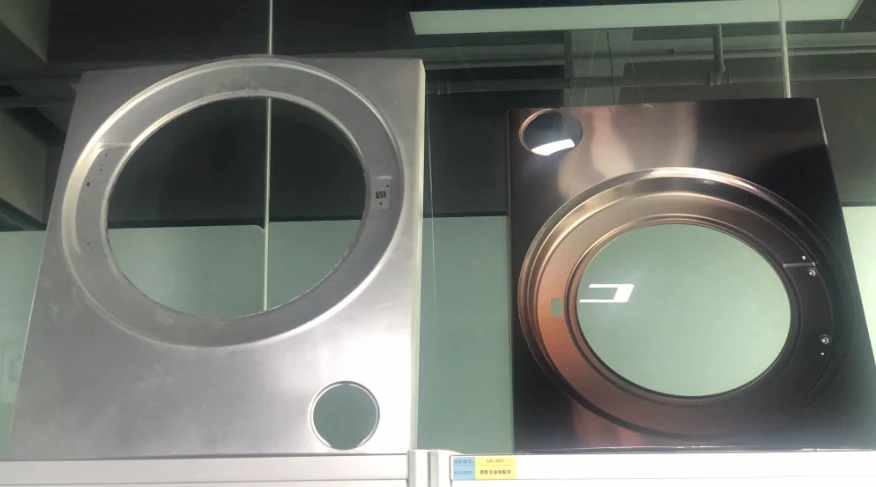
Equipment and samples from the Huasheng Precision company presentation. Laser cutting, NCT punching, bending, pressing, welding and assembly are reviewed against the requested drawing.
Frequently asked questions
What is the minimum bend radius for 6061-T6 aluminum sheet?
United Aluminum lists 1t at 1/64 in and 1/32 in, 1½t at 1/16 in and 2½t at 1/8 in for a 90-degree cold bend in a press brake with air-bend dies. The same source notes that other bending operations and tooling condition can require a larger radius or permit a smaller one.
What is the minimum bend radius for 5052-H32 aluminum sheet?
United Aluminum lists 0 at 1/64 in and 1/32 in, 1t at 1/16 in and 1½t at 1/8 in for a 90-degree cold bend. 5052-O is listed at 0 up to 1/16 in and ½t at 1/8 in.
What K-factor should I use for copper?
We did not find a published K-factor table specific to copper. Machinery’s Handbook gives a 90-degree bend formula for soft copper and soft brass, L = 0.55T + 1.57R, which corresponds to a K-factor of about 0.35 by our calculation. Its formula for half-hard copper and brass, L = 0.64T + 1.57R, corresponds to about 0.41. Confirm the value with a test bend in the actual material and tooling.
What K-factor should I use for aluminum?
The generic chart published by The Fabricator gives 0.33 to 0.38 for air bending with an inside radius up to one thickness, 0.40 to 0.43 from one to three thicknesses, and 0.50 above that. Machinery’s Handbook groups aluminum with soft steel in a formula that corresponds to about 0.41. These are starting values; a test bend gives the value for your tooling.
Is the minimum bend radius of 304 stainless steel 0.5t?
ASTM A666 requires annealed 304 sheet to withstand a 180-degree free bend around a diameter equal to one thickness, which is an inside radius of 0.5t. That is a material acceptance test, not a forming recommendation for a production part. Springback, surface finish and tooling should be reviewed separately.
Does Huasheng guarantee the radii in this chart?
No. The chart collects published reference values and names the source of each one. Send the material, temper, thickness and inside radius, and we review the bend against the drawing and the tooling to be used.
Technical references
- SSAB: bending conditions and terminology
- Autodesk: sheet metal rules and K-factor
- United Aluminum: recommended minimum bend radii for aluminum sheet
- American Steel & Aluminum: ASTM A1011 bend guidance
- SSAB: Docol dual-phase steel datasheets
- Aurubis: Cu-ETP (C11000) strip datasheet
- The Fabricator: analyzing the k-factor in sheet metal bending
- Machinery’s Handbook, 31st edition: bend allowance formulas
- ASTM A666-10 and ASTM B265-08b (bend test requirements)
A reference supplier’s equipment settings or material limits are not statements of our manufacturing capability.